




 View Count:9
 Date:2026-10-30
Where does garden tool mould come from, and how do you prevent it? From the overmoulded grip and the carton liner, not the blade, and a rejected export lot is a full container turned back at the buyer’s dock. Dose the grip compound with iHeir-JS117 at 0.5%-1.0% of compound weight, then oil the blade and pack it with iHeir-D paper at 0.1-0.2 g of active content per sheet. This article covers both stages, the blade sequence and the release test.
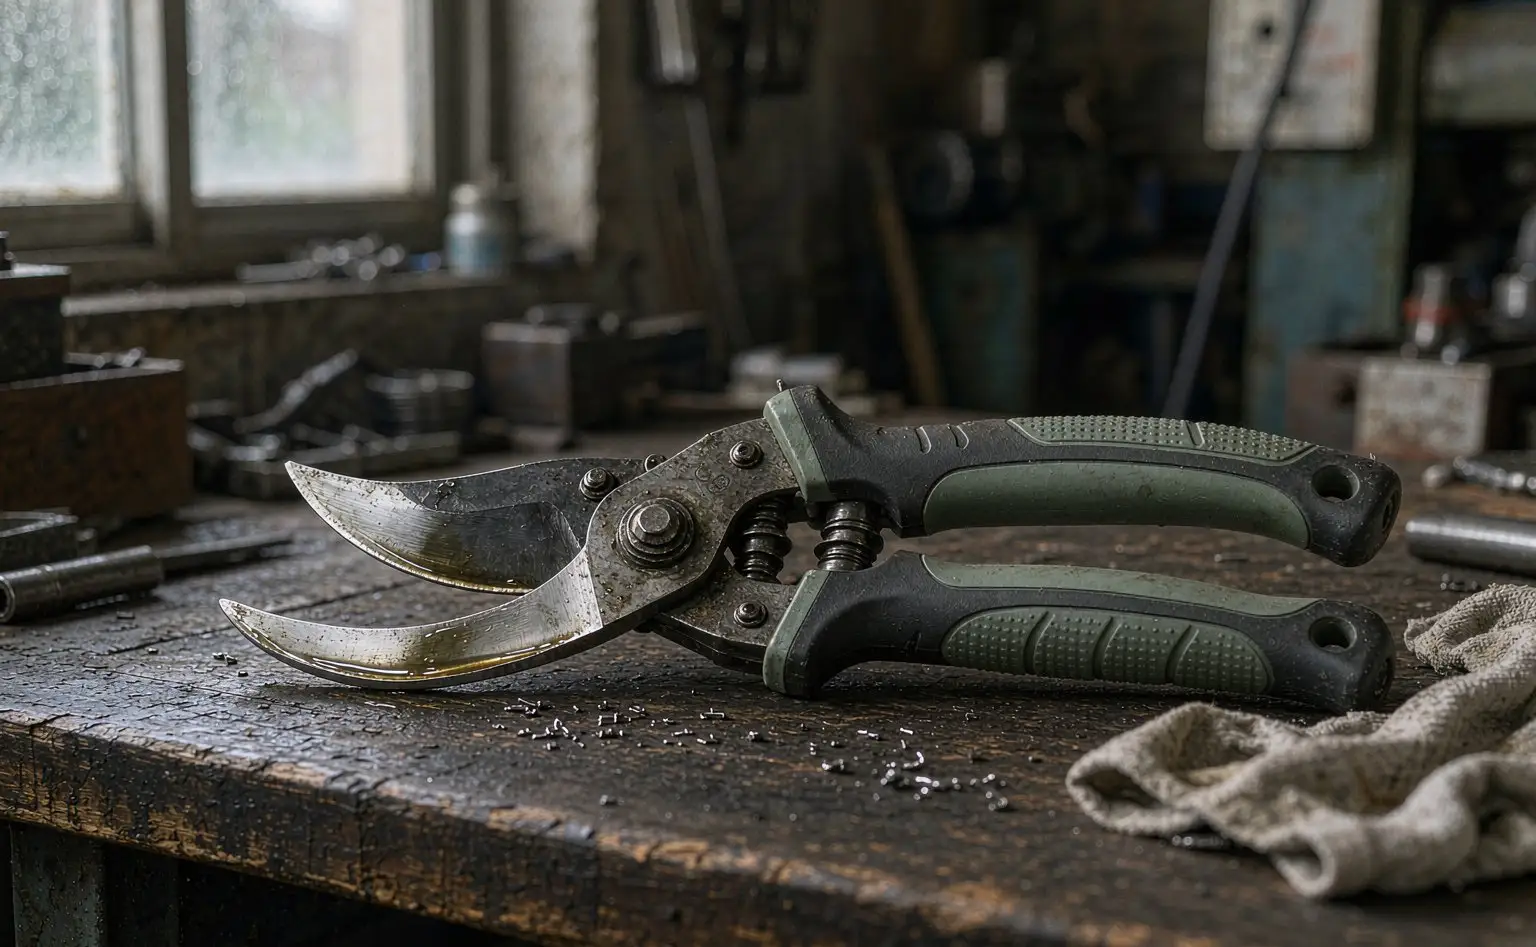
1. Mould starts on the grip and in the carton liner
A garden tool is a fixed material set: 65Mn or SK5 blade, PP or ABS handle, TPR two-colour overmoulded grip, carton with an instruction card. Metal does not grow mould; rust starts at the edge and the grind, which is a separate problem. But a buyer who opens a carton and sees a pale grip and a dull blade grades both as cosmetic defects.
The first location is the grip. TPR/TPE carries white oil, softener and filler, and the non-slip ribs collect sweat and dust. Three to five days in a humid shop and a grey speck appears at the base of the rib. The grip is the first thing a buyer touches, and a speck is a return.
The second is the handle cavity and the carton. A PP handle is a half-closed cavity: water left from moulding and moisture carried in at assembly cannot leave, and the day-night swing on a sea leg condenses it on the inner wall. Carton, instruction card and colour sleeve take up moisture and become the bed; a full container in a still store is worse than the shop floor.
2. Grip, blade and packing are handled separately
The table lines up the four parts. The grip is dosed on compound weight, the paper on sheets and active content, and the two are not convertible.
| Part | Material | Product and level | Stage | Control point |
|---|---|---|---|---|
| Overmoulded grip | TPR/TPE compound | iHeir-JS117 0.5%-1.0% of compound weight | Dry blend or compounding | Even mixing, melt temperature respected |
| Handle | PP/ABS | No additive, drying and blowing only | Dry the pellets before moulding | Moisture per the process card |
| Blade | 65Mn or SK5 carbon steel | Rust-preventive oil, thin and even | After grinding, cleaning and drying | No pooling at the edge |
| Carton and export | Liner, instruction card | iHeir-D 0.1-0.2 g per sheet | Packing and loading | Paper facing in, box sealed |
Two boundaries. The PP/ABS handle does not need an additive: it fails by moisture distortion and appearance, not by mould, and the money is better spent on the grip and the packing. And the paper is not a desiccant: it releases active content into a closed space to suppress organisms, it does not absorb water, and free water in the carton has to be blown out first.
3. Grip compound: the powder goes in at the dry blend or compounding
The grip uses iHeir-JS117 plastic anti-mould powder at 0.5%-1.0% of grip compound weight. Active content is above 97%, bulk density 380 kg/m³, mean particle size D50 around 110μm. It is insoluble in water, so a wet grip or repeated wiping does not leach the additive out.
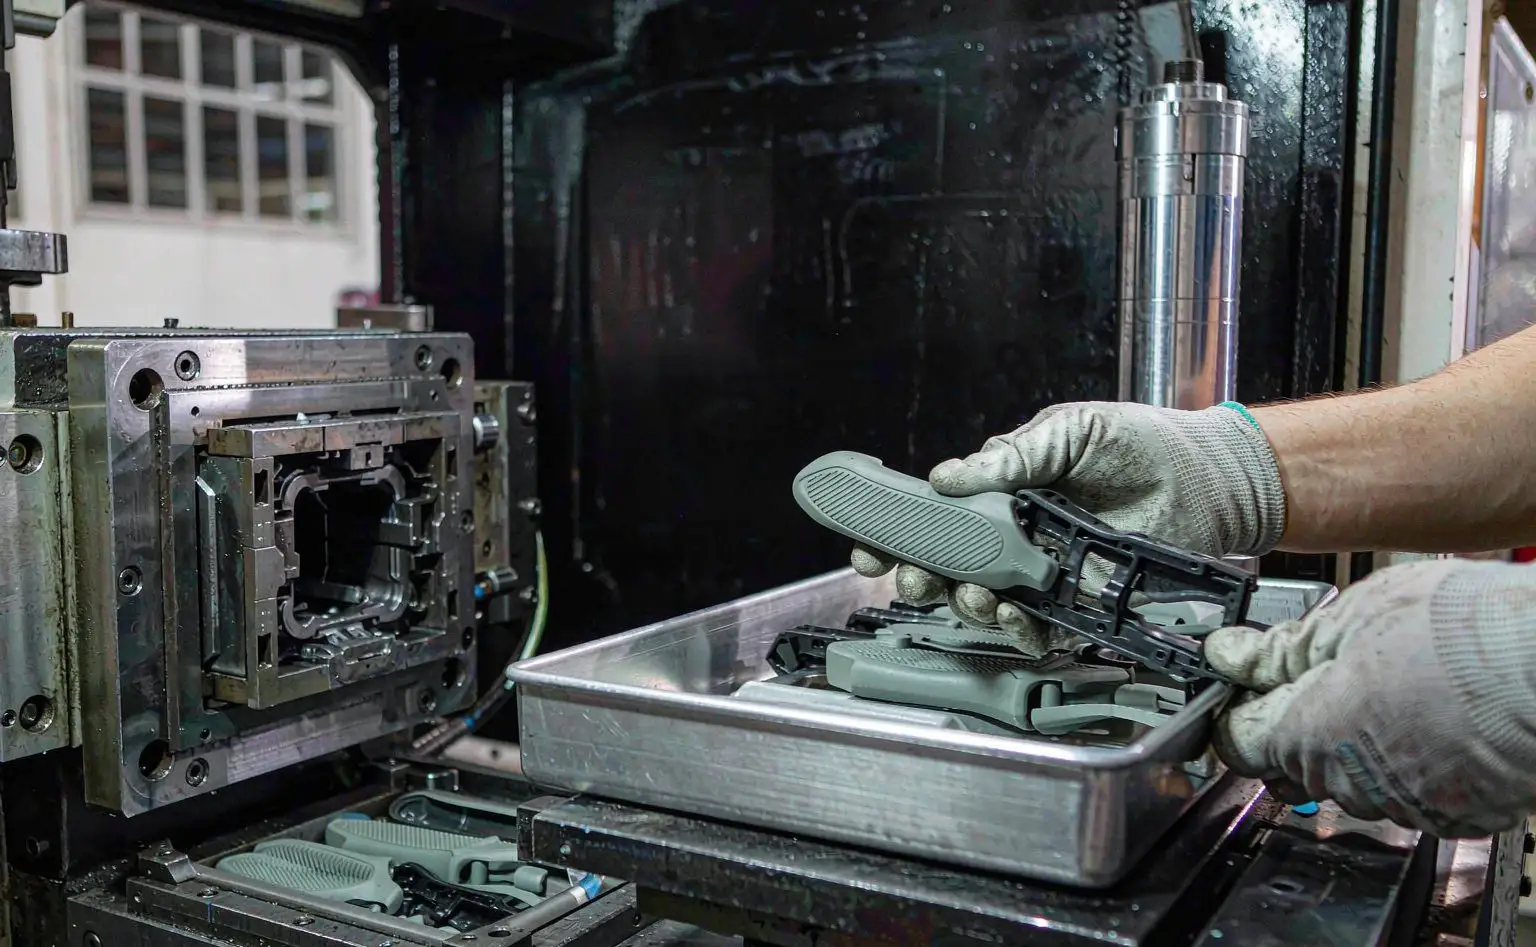
Two ways in. If you compound in house, it goes into the high-speed mixer with the other powders for 8-10 minutes at the dry-blend stage; if the compound is bought in or you run a colour masterbatch, blend it on a twin-screw at pelletising and mould the grip afterwards. Do not hand-scoop powder into the machine hopper: the concentration drifts and the shop gets dust. Overmoulding is a second shot onto the hard handle, so keep the melt temperature the process already uses.
Three points. Ribs: a deep non-slip pattern holds water after demoulding, and blowing it dry does more than adding dose. Regrind: grips often carry regrind, and a high ratio calls for the top of the range at 1.0%. Feel: above 1.0% softness shifts slightly, so trial a sample where grip feel is specified.
4. Blade oiling and the paper in the carton
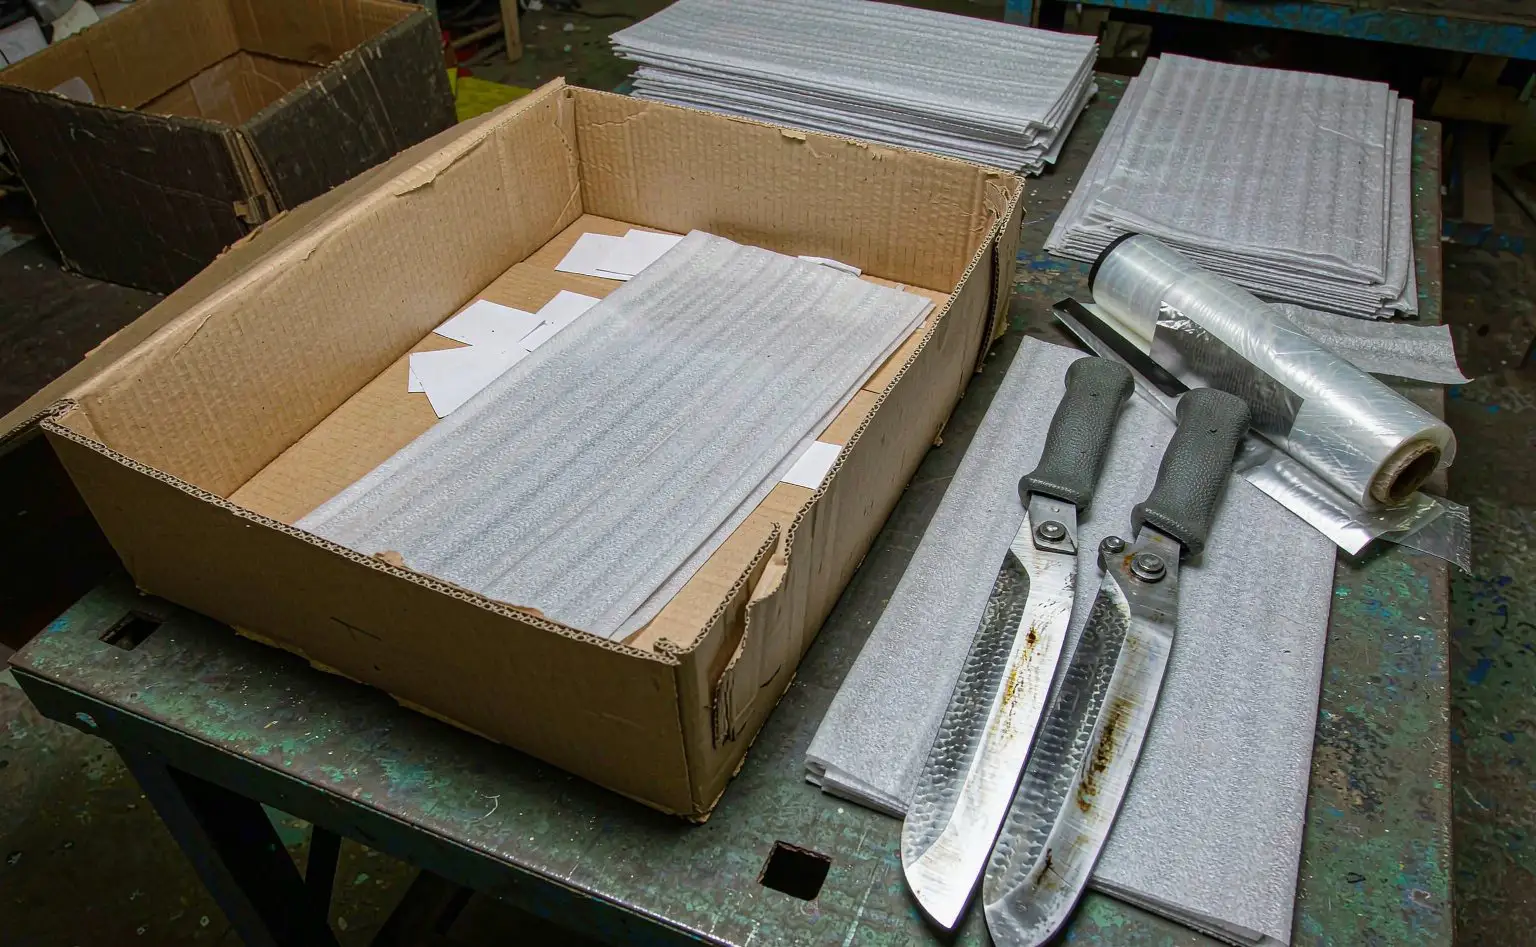
The blade sequence is grind, clean, dry, oil, sleeve. The oil goes on thin and even, with nothing pooling at the edge, and the order cannot be reversed: sleeve first and the paper takes up the oil instead. The oil is not our product, but it decides whether a blade still looks saleable after two months in a container; the selection logic is in choosing anti-rust and desiccant protection.
Inside the carton the product is iHeir-D gas-phase anti-mould paper, 0.1-0.2 g of active content per sheet, solids 70%±5, 25kg per drum, one year shelf life. It is a coated paper, so position and closure decide the result: it goes against the carton wall with the face towards the grips and the box is sealed. Sheet count follows carton volume and piece count; the usual pattern is one sheet against the wall plus a small one at the grips, settled by a packing trial.
One test you have to run first: metal compatibility. In damp conditions the paper can corrode poor-quality metal parts, and a garden tool carries a carbon steel blade, rivets and a spring. Take three times the normal sheet count, seal it in a bag with blades and rivets from the same batch, hold 7 days at 40℃/90% RH, then open and look for a dull edge and darkened rivets. If it fails, change the packing structure rather than forcing the paper in.
5. Assembly, finished-goods store and export loading
Three things at assembly: blow the ribs dry after demoulding; blow dry air through the handle cavity; hold shop humidity at 60% RH or below.
In the store: cartons on pallets, off the floor and 10cm off the wall, 60% RH or below, first in first out. Six-month stock is where trouble shows, so open two cartons before an export shipment and check grips and blades.
Leave an air path in the container; the condensation logic is in condensation in sea freight containers. Release at three levels: grip parts to GB/T 1741 or ASTM G21, sampling at the rib; whole cartons for 30 days at 30℃/85% RH, checking grips, blades and the instruction card; and, where a buyer asks for bacterial data, ISO 22196 or GB/T 20944.3.
6. Questions on tacky grips, oil order and mouldy lots
Q: Will the powder make the grip tacky or fade it?
JS117 is a powder and insoluble, so at a normal dose it does not change the surface. Tackiness usually comes from a high regrind ratio, white oil blooming or too hot a melt. Run a control: half the batch dosed, half not, moulded together and both into a 70℃ oven.
Q: Oil first or paper first?
Oil first, let it dry, then pack with the paper. Reverse the order and the paper drinks the oil, and both stages fail; do not press the paper onto a wet film either.
Q: Can a lot that already shows mould ship?
Surface bloom at the base of the ribs can be wiped, then feel and appearance re-checked; where mould has gone into the rib base and a mark stays, the grip part is replaced. A reworked lot needs the grip dosing and the packing stage again; wipe only, and it returns within two weeks in the bag.
Four points to take away: dose the grip compound with iHeir-JS117 0.5%-1.0% of compound weight at the dry blend or compounding for 8-10 minutes, and go to 1.0% where the regrind ratio is high; oil the blade after grinding and sleeve it only once dry; put iHeir-D paper at 0.1-0.2 g per sheet into the carton by piece count, after a three-fold metal compatibility test; hold the store below 60% RH, leave an air path in the container and release on 30 days at 30℃/85% RH. A 1kg powder sample and 20 sheets of paper can go out for a machine trial first; MOQ and lead time are on the iHeir-JS117 product page.


