




 View Count:66
 Date:2026-10-08
Where should eyeglass case mould treatment be fixed on two points? A case is built from an EVA shell, a leather or PU outer face and a velvet liner, and the mould starts on the liner and the sponge interlayer, so a single spray on the finished outside never reaches the inner face. The EVA shell takes iHeir-FP foam antimicrobial agent at 0.5%-1.5% on foam weight at the moulding stage, and the velvet liner takes iHeir-BJ textile mildew inhibitor at 2%-3% o.w.f. in the padding bath. This article covers the two dosing points, the storage control and the figures.
1. Where the mould comes from: shell, liner and interlayer are three stages
A case looks like one hard shell, but it is at least three materials. The EVA shell is a foamed part, faced with cloth or leather outside and lined with velvet inside, with a sponge or sponge-composite layer in between; the outer face may be PU synthetic leather or real leather. Mould starts almost always at the innermost point: the velvet liner is dense and takes up moisture quickly, the sponge interlayer is full of cells and holds damp without releasing it, and the two sit with no air movement, so a case held a few months in store grows mould on the liner face.
The shell itself does not absorb water, but it locks the damp inside. Once the case is closed, the liner and the sponge interlayer form a small sealed space, ventilation cannot carry the damp away, and this is why a case moulds more readily than a plastic box of the same size.
On the line, a U-shaped process moulds the EVA shell first, fits the liner second, and wraps the outer face last. The shell takes the agent with the foam compound at moulding, the liner is treated in the finishing stage, and the outer face follows its own leather system. Merge the three into one spray on the finished case and only the surface is covered.
2. The two dosing points at a glance: shell and liner
The table lines up the part, the stage, what is treated, the product, the figures and the points to watch, so it can serve as the first draft of a process card.
| Part | Stage | Treated item | Product | Figures | Points to watch |
|---|---|---|---|---|---|
| EVA shell, sponge interlayer | Foaming / moulding | Foam compound | iHeir-FP foam antimicrobial agent | 0.5%-1.5% on foam weight | In with the foam compound; stable from pH 1-11, check compatibility with the foaming aids on a small sample |
| Velvet liner | Padding | Dry fabric weight | iHeir-BJ textile mildew inhibitor | 2%-3% o.w.f. | Bath 21-50 degrees, pH 4.5-8.5; cationic, never with an anionic aid |
| Sponge composite layer | Lamination | Composite | Same grade as the shell | On the foam-compound figure | Treat with the shell in the same batch, so the interlayer is not missed |
| Outer face (PU / leather) | Wrapping | Leather system | By the leather figure | Not set here | A third system; its figures must not be borrowed across |
| Finished store and packing | Stacking / carton | Air in the stack | Humidity control only | Below 60% relative humidity | Sealed and still; sheets by stack, and dry the goods before cartoning |
Five rows, one conclusion: the shell is figured on foam weight and the liner on dry fabric weight, so the two denominators and bands differ, and the store takes no agent at all, only humidity control.
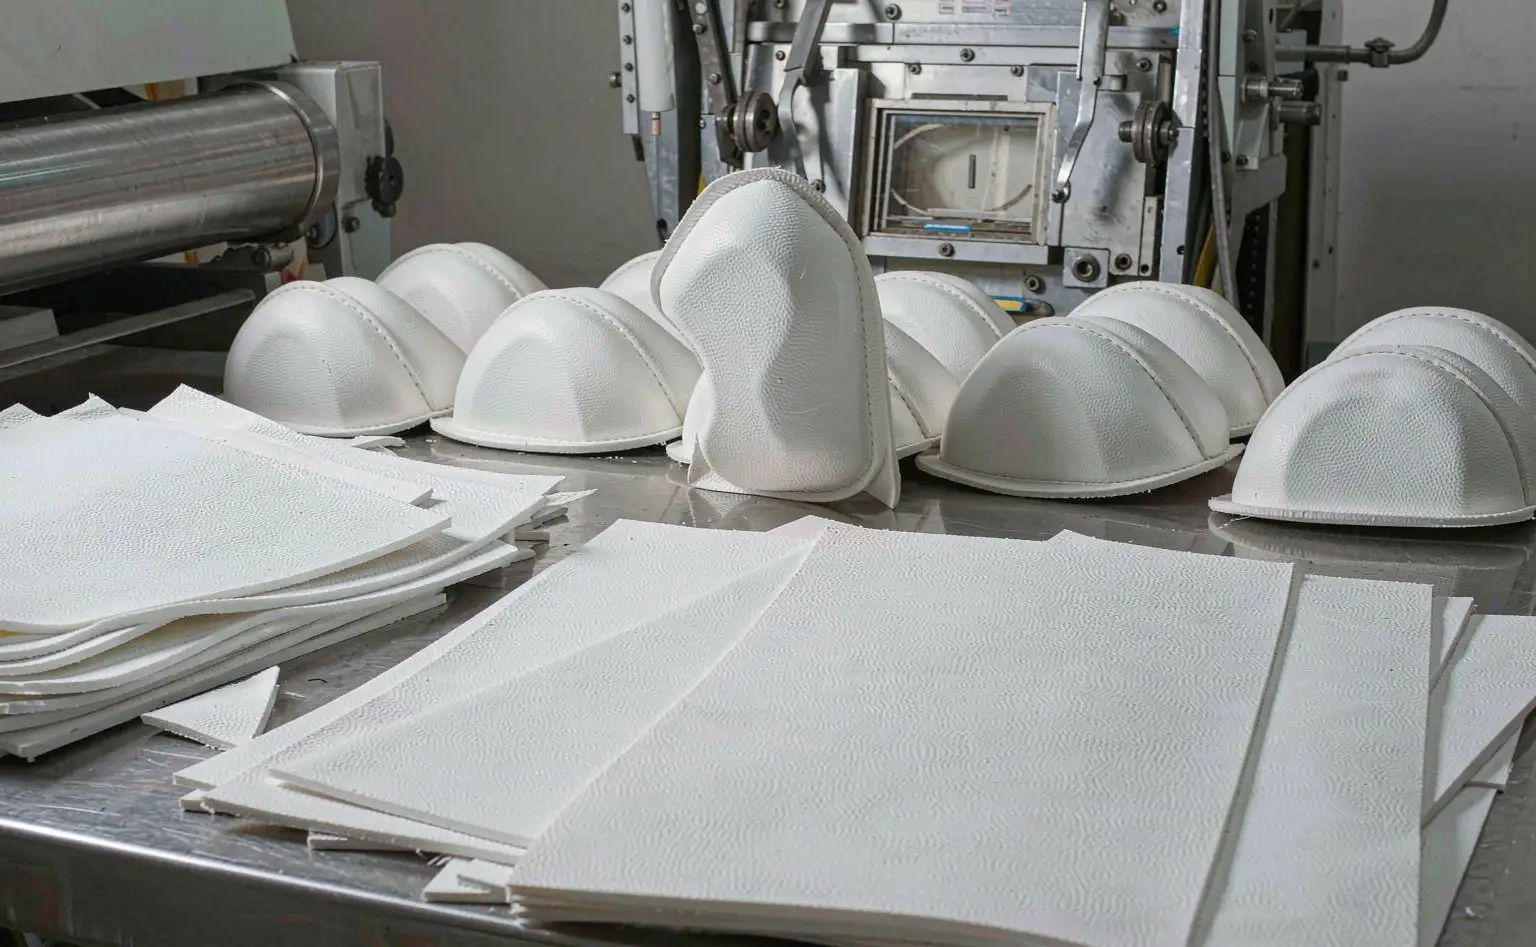
3. The EVA shell: FP in the foam compound at 0.5%-1.5%
The shell line is completed at the foaming and moulding stage. Add iHeir-FP foam antimicrobial agent at 0.5%-1.5% on foam plastic weight, in with the foam compound so it disperses through the system. It is stable from pH 1-11, so the mildly acidic or neutral EVA foam formulations commonly used are all compatible, and the antimicrobial rate reaches 99.99% with a sensitisation rate of 0, which leaves a safety margin on an item worn against the face. The additive is bonded inside the foam, so cutting, laminating and edge trimming will not rub it off.
Three details. First, the figure is on total foam weight, regrind included, so any change in the regrind ratio means recalculating, and high-regrind batches belong at the top of the range. Second, a foam compound carries many aids, so premix with the main foam material for even dispersion before foaming, since powder fed straight in agglomerates locally. Third, run the sponge composite layer with the shell in the same batch rather than protecting the shell and missing the interlayer, which is the part that holds most damp. See selecting a mould inhibitor for real leather and PU leather for the grade.
4. The velvet liner: BJ in the padding bath at 2%-3% o.w.f.
The liner line is completed at the padding or dipping stage. Add iHeir-BJ textile mildew inhibitor at 2%-3% o.w.f. on dry fabric weight, with the bath held at 21-50 degrees and the pH between 4.5 and 8.5, ideally near 6. Premix it with 9-13 times its volume of water and add it in portions to avoid a local concentration spike; hold the wet pick-up at 70% and add 0.1% of a hydrophilic agent to improve the hand. After normal drying and setting the anti-mould layer is fixed on the fibre, and 2% broadly supports a year or more of protection while 3% reaches two to three years.
Three details. First, BJ is cationic, so it must never share a bath with an anionic aid; if the liner also needs softening or antistatic finishing, check the ionic nature of those aids before fixing the bath order. Second, use soft water, since calcium and magnesium in hard water weaken its fixation on the fibre. Third, watch for shade shift on pale liners and run a small sample before a full bath.
5. Finished store and export packing: the stage no agent is dosed
The store matters just as much. Bagged cases are stacked tight, the sealed inner space has no air movement, and ventilation will not carry damp out of the core of a stack; place gas-phase sheets by stack, keep them apart from the goods with liner paper, and hold the store below 60% relative humidity. For batches held a long time, bring the moisture of the goods down before cartoning, because condensation once the carton is sealed is the ignition point.
Packing can also use desiccants by carton type. A sea voyage is long and the day-night temperature swing is wide, so condensation inside a sealed carton is harder to control than in a warehouse, and desiccant sticks matched to the carton stabilise the humidity. See how to choose anti-mould packaging paper for the practice.
6. Questions that come up: one figure for both, or a spray afterwards
Can the shell and the liner share one loading? No. The shell is figured at 0.5%-1.5% on foam weight and the liner at 2%-3% o.w.f. on dry fabric weight, so copying one number either wastes material or falls short.
Can a spray over the finished case make up for it? It reaches the exposed surface only, leaving the velvet liner and the sponge interlayer inside untouched, and rubbing and wiping take the surface layer off.
Can extra loading on the liner cover a long spell in store? No. Damp in storage is an environment problem, not a concentration problem, and extra loading only raises cost. Hold the store below 60% relative humidity and dry the goods before cartoning.
Two dosing points carry the work: the EVA shell and the sponge interlayer go in with the material at the foaming stage (iHeir-FP at 0.5%-1.5% on foam weight, stable from pH 1-11), and the velvet liner is padded in the bath (iHeir-BJ at 2%-3% o.w.f., bath 21-50 degrees, pH 4.5-8.5, cationic, never with an anionic aid), while the store and export packing preserve both by humidity control and gas-phase sheets. Test the long-term growth by ASTM G21 and hold a complete sample per batch, since testing the shell alone or the liner alone does not count. Samples and TDS sheets are available for a trial on your own line.


