




 View Count:30
 Date:2026-10-17
Which layer of a yoga mat needs the mould treatment, the TPE foam or the embossed surface? A mat that takes up moisture in the foaming shop while its face keeps sweat and release residue reaches the customer with spots, and the batch comes back as a claim. iHeir-FP foam antimicrobial agent goes into the foam at 0.5%-1.5% of foam weight, and iHeir-ECO plastic antimicrobial agent goes into the embossed surface layer at 0.3%-1.0% of that layer’s polymer. This article covers where each is dosed, the temperature window and the storage rules.
1. Yoga mat mould: the foam and the embossed face are two separate bills
A mat is normally a core plus a face. The core is a TPE, XPE or EVA foam sheet, the face is an embossed or coated anti-slip skin, and the two are bonded before being cut to length and rolled. Foam is full of closed cells, so its real surface area is far larger than it looks, and when shop humidity rises the sheet takes up water while it is stacked and wound. The face is dense, but the surface treatment in front of the embossing station stands open to shop air, and whatever sits on it gives micro-organisms somewhere to start.
The two are not the same problem. Foam is a thick material: the additive has to be inside it to mean anything, and a surface spray stops at the skin. The face is thin: mixed into the polymer of that layer, the additive distributes evenly, but the processing temperature has to be watched, because embossing and bonding run hotter than foaming and the additive system must survive that window. Different dosing stages, different bases, different temperature windows — pooled into one figure, one of the two layers will always be underdone.
2. The foam layer and the embossed face compared
The table lines up the material, the dosing stage, the figure and the points to watch for each layer, as a first draft of the process card.
| Layer | Material | Dosing stage | Figure | Points to watch |
|---|---|---|---|---|
| Foam layer | TPE, XPE or EVA foam | Blended with the foam compound at the mixing stage, then foamed | iHeir-FP at 0.5%-1.5% of foam weight | Stable from pH 1 to 11; a liquid that disperses in water at any ratio, so stir before mixing |
| Embossed face | Face polymer or coating | Compounded into a masterbatch, then embossed or coated | iHeir-ECO at 0.3%-1.0% of that layer’s polymer | Heat stable to 240℃, keep processing below 320℃; mix well before forming |
| Bonding and embossing | Two semi-finished webs | Control moisture and residue on the face before bonding | Roller temperature on each process; relative humidity below 60% | A face bonded while damp seals that water into the middle layer |
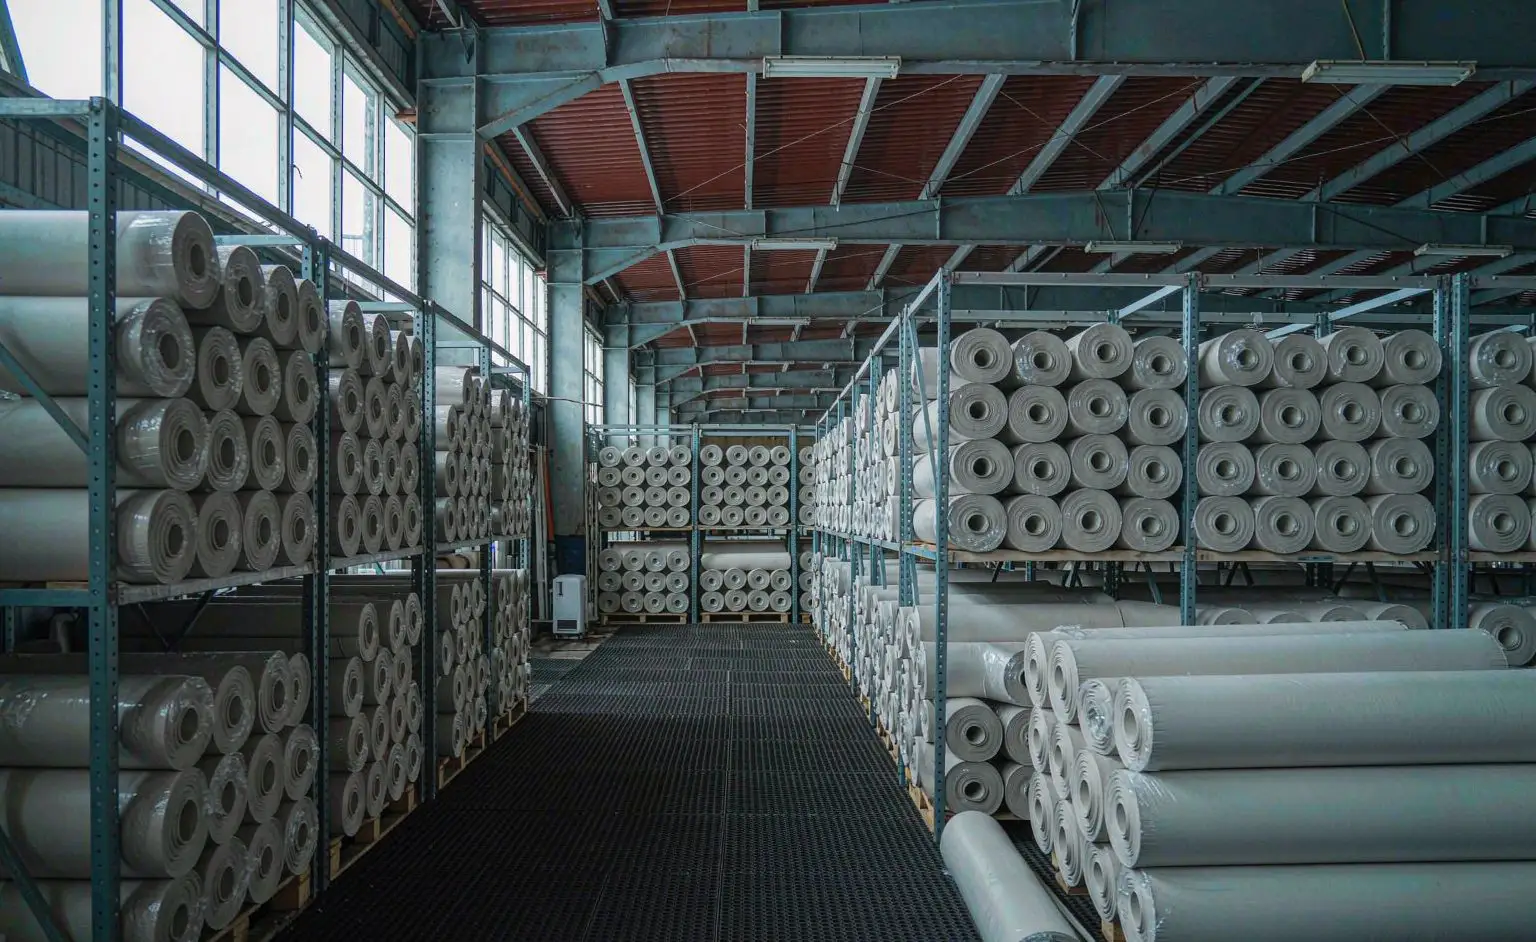
| Finished rolls and store | Finished roll | Humidity control, upright stacking, sealed roll ends | Relative humidity below 60% | The core collects moisture first; keep pallets off wall and floor, first in first out |
The first two rows are two separate dosing lines, the third looks after the interface before bonding, and the fourth is the storage discipline behind them. Miss any one and the problem only shows when the customer opens the roll or lays the mat out.
3. Foam layer: FP at 0.5%-1.5% of foam weight
The foam uses iHeir-FP foam antimicrobial agent at 0.5%-1.5%, counted on the weight of the foam compound, not on the finished mat. It is a clear to pale yellow liquid with a specific gravity of 1.045-1.055, disperses in water at any ratio and stays stable from pH 1 to 11, so it suits an acidic EVA system as well as the neutral TPE and XPE systems.
Dose it at the mixing stage: blend the agent with the foam compound, then run the extrusion and foaming, so the additive travels with the melt into the body of the sheet. The higher the expansion ratio and the thicker the sheet, the longer the path the additive has to travel, so allow extra mixing time. Parts that only get a surface spray look clean at the time, but as soon as they are cut or rolled and a fresh cross-section is exposed, the inside is still bare. On safety, acute oral LD50 is above 5000 mg/kg with a skin sensitisation rate of zero, so normal shop protection is enough.
Two notes on the figure. The 0.5% end is a floor: thick sheets and long storage cycles justify moving up, while 1.5% is the normal ceiling, beyond which extra cost buys very little. A single plastic surface antimicrobial test is a cheaper way to settle the level than piling on more additive.
4. Embossed face: ECO at 0.3%-1.0% of that layer’s polymer
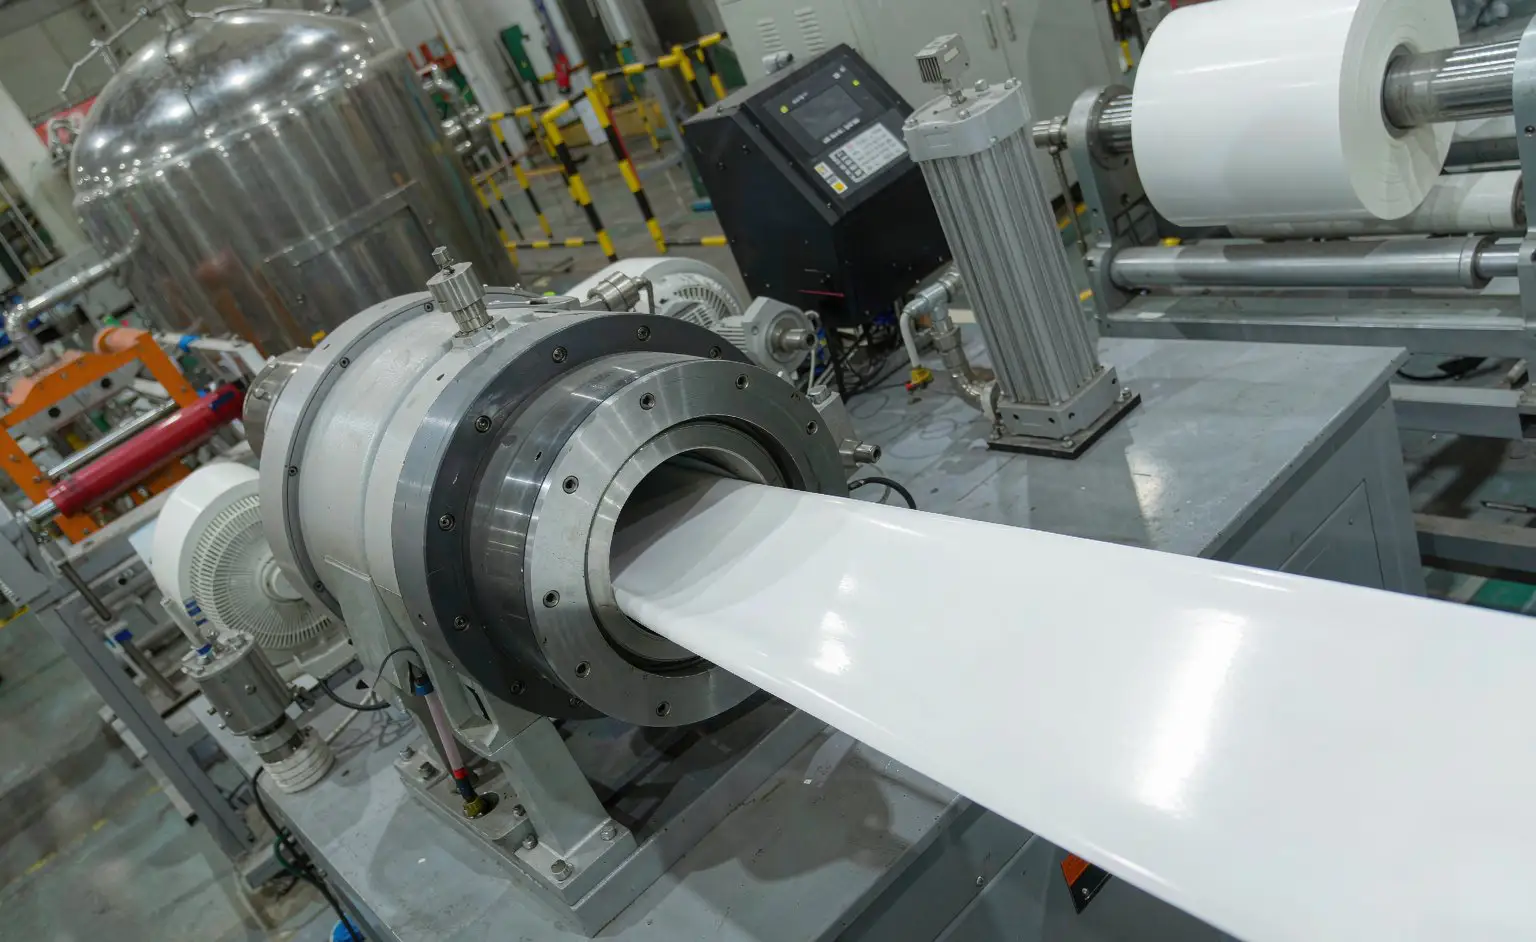
The face uses iHeir-ECO plastic antimicrobial agent at 0.3%-1.0% of that layer’s polymer: 0.3%-0.5% in a PE or PP system, 0.3%-1.0% in PU, and 0.5%-1% in PVC. It is a grey-white powder of 100% purity, added as a masterbatch at the plasticising or mixing stage and compatible with normal extrusion and coating lines. Because the face is thin, an evenly dispersed additive protects the whole surface and lasts far better than a spray applied afterwards.
Temperature is the critical point here. ECO is heat stable to 240℃ and processing should stay below 320℃, because overheating volatilises the active and wastes the dose. Check the temperature on both the embossing and the bonding rollers, especially close to the roller face, and step up to a higher temperature grade where necessary. This is an internal additive, and the choice between masterbatch and powder is set out for plastic anti-mould masterbatch or powder.
5. TPE is temperature sensitive: where to dose and how wide the window is
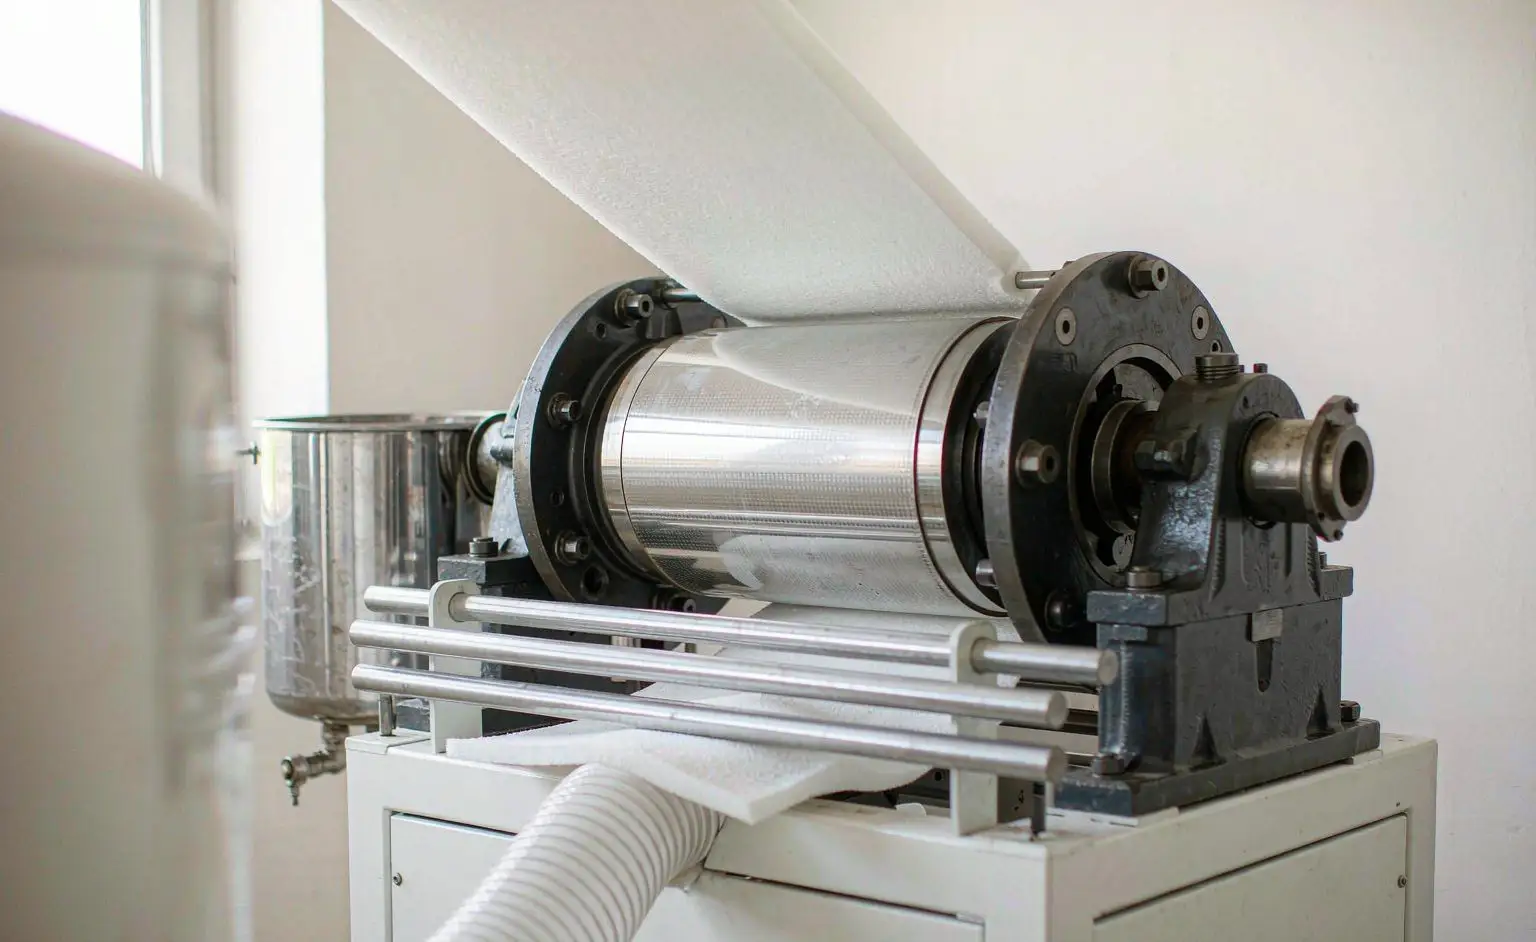
TPE is a thermoplastic elastomer that sets through physical cross-linking, so once the temperature runs away the sheet sags and loses its rebound, and an additive that goes in cannot be held. The rule for this stage is to dose before foaming: the agent is blended with the compound at the mixing temperature and travels with the melt through foaming and cooling, so no second addition is needed in a hot stage. That keeps the agent away from the high-temperature steps and still spreads it evenly through the sheet.
Set the window to the material. TPE and EVA mix at lower temperatures than XPE, and it is better to extend the mixing time than to raise the temperature to speed dispersion up. Bonding and embossing are the hottest points on the line, so the additive system and the process parameters have to be confirmed together there — if the agent cannot take it, no amount added at the foaming stage will survive. Dosing figures and compatibility for foam systems are set out for foam and elastomer antimicrobial dosing in EVA, EPS and TPU.
6. Questions: is one layer enough, and can a surface spray replace internal dosing
Is dosing the foam enough, with the embossed face left untreated? Not advisable. The face is what meets the outside world once the mat is laid out, and with nothing in it, friction and wiping during rolling and unrolling leave contamination on the surface. Once the two layers are bonded, moisture at the interface cannot escape either, and the face is usually where it shows first. Both layers together are what keeps water and organisms out.
Can a spray on the finished mat replace internal dosing? No. A spray stops at the skin and misses cut edges, embossed grooves and the core; on a large roll the inner layers cannot be reached at all. Internal dosing puts the protection into the material, so a freshly cut cross-section is protected too, which a spray cannot do. Samples and TDS are available for both products, and we can run a trial against your existing compound.
Four points carry the work. The foam takes iHeir-FP foam antimicrobial agent at 0.5%-1.5% of foam weight, blended at the mixing stage before foaming. The embossed face takes iHeir-ECO plastic antimicrobial agent at 0.3%-1.0% of that layer’s polymer as a masterbatch, with processing kept below 320℃. Moisture on the face and the sheet is controlled before bonding below 60% relative humidity. Finished rolls are stood on end, off wall and floor, with the ends sealed.


